About

Nijal Mineral and Chemical Industries Pvt. Ltd. (NMACIPL) is a leading manufacturer and exporter of high-quality manganese-based industrial chemicals and powders. Founded in 2010, we’ve spent more than two decades perfecting the science and craft of chemical production—serving battery manufacturers, water treatment facilities, ceramics producers, glass makers, pharmaceutical companies, and industrial distributors across India and international markets.

Established since 2010, and we are committed to development.

About Nijal Mineral and Chemical Industries Pvt. Ltd. (NMACIPL)

20+ Years of Industrial Manufacturing Excellence in Manganese-Based Chemicals

In 2010, founders Ashik Shah and Alka Shah established Nijal Industries with a clear vision: to become a reliable manufacturer of high-quality manganese chemicals for India’s growing industrial sector. What started as a focused operation has evolved into a manufacturing powerhouse that serves some of the country’s most demanding industries.

Our growth wasn’t accidental. It was built on three foundational principles that continue to guide us today:

  1. Quality Above Everything From day one, we invested in equipment and processes designed to ensure consistency. We understood that our customers’ success depends on reliable products, and we took that responsibility seriously. This commitment remains unchanged 20+ years later.
  2. Focus on Specialization Rather than chase every industrial chemical market, we focused deep on manganese-based chemistry. This specialization allowed us to become experts—understanding every nuance of production, every application variation, every customer need in our domain.
  3. Genuine Partnerships We view our customers not as transactions but as partners. When you source from Nijal Mineral and Chemical Industries Pvt. Ltd. (NMACIPL), you’re working with people who understand your industry, anticipate your needs, and are invested in your success.
OUR JOURNEY

Key Milestones in Our Manufacturing Evolution

2010

Foundation

Ashik Shah & Alka Shah

Established with a focus on high-quality Manganese Dioxide manufacturing for the Indian industrial market.

2015

Export Growth

Global Routes & Mumbai Sales Office

Established international export supply chains and opened a dedicated Mumbai sales office for domestic coordination.

2018

Facility Expansion

Halol, Gujarat (500,000 sq ft)

Expanded footprint with substantial investments in advanced furnace technology and high-precision quality control systems.

2020

Production Scaling

60,000 MT Annual Capacity

Installed additional furnaces and Raymond mills; expanded into Manganese Oxide, Manganese Sulphate, and specialty oxides.

2023

Technology Upgrade

Automation & R&D

Implemented modern automation process control systems and upgraded laboratory facilities for rigorous QA and R&D.

2024

Market Leadership

Multi-Sector Supplier

Trusted partner across battery, water treatment, ceramics, glass, and pharma sectors backed by year-round inventory infrastructure.

2025

Private Limited & Continued Excellence

Corporate Transition & Sustainability

Converted to Private Limited status; operating at 60,000 MT annual capacity with an active roadmap for sustainable green growth.

WHO WE ARE TODAY

Nijal Mineral and Chemical Industries Pvt. Ltd. (NMACIPL) Today: Manufacturing at Scale

Today, Nijal Mineral and Chemical Industries Pvt. Ltd. (NMACIPL) operates as a specialized high-quality manufacturer serving multiple industrial sectors. Our current state reflects decades of investment in equipment, people, systems, and commitment to excellence.

The Team

Nijal Mineral and Chemical Industries Pvt. Ltd. (NMACIPL) is led by experienced operators who understand manganese chemistry, manufacturing processes, and industrial customer needs. Our management team brings decades of combined experience in chemical manufacturing, technical operations, quality assurance, and B2B sales.

Our production team includes skilled operators trained on advanced equipment and committed to quality at every stage. We invest in continuous training and development because our people are our greatest asset.

Our sales and support team understands the technical requirements of our diverse customer base—from battery manufacturers to water treatment specialists—and provides the guidance and service that builds long-term partnerships.

The Facility

Our manufacturing facility spans 500,000 square feet across multiple dedicated production areas. Each section is designed for specific processes: raw material handling, furnace operations, grinding and milling, quality testing, and packaging.

The facility has been progressively upgraded with modern equipment, automation systems, and environmental controls. We maintain it to standards that reflect our commitment to quality and safety.

The Capacity

Annual production capacity of 60,000 MT is distributed across:

  • 7 Furnaces: 1,800 MT/month production
  • 4 Raymond Mills: 4,000 MT/month grinding capacity
  • 4 Reactors
  • Multiple Support Equipment: Material handling, quality testing, and packaging

This capacity allows us to handle bulk orders, maintain inventory for consistent availability, and respond to customer needs with flexibility.

MANUFACTURING EXCELLENCE

How We Manufacture Manganese Products

Manufacturing quality manganese chemicals is as much science as craft. Our process reflects decades of refinement, modern equipment, process control, and unwavering quality standards.

Raw Material Selection

Raw Material Selection

Quality products begin with quality inputs. We maintain rigorous incoming inspection protocols for all raw minerals. Every batch is tested prior to production to strictly meet specifications.
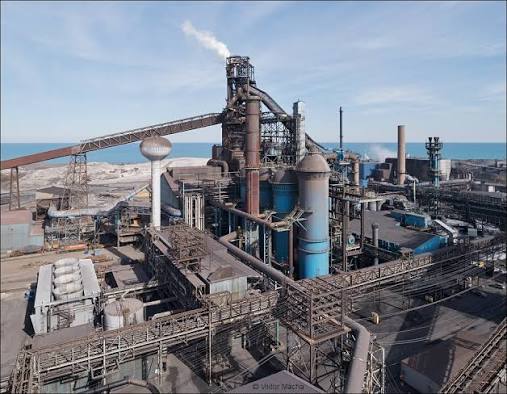
7 Industrial Furnaces

Furnace Operations

Our 7 furnaces operate continuously under controlled conditions. Temperature, timing, and atmosphere are regulated by trained operators to ensure consistent product characteristics.
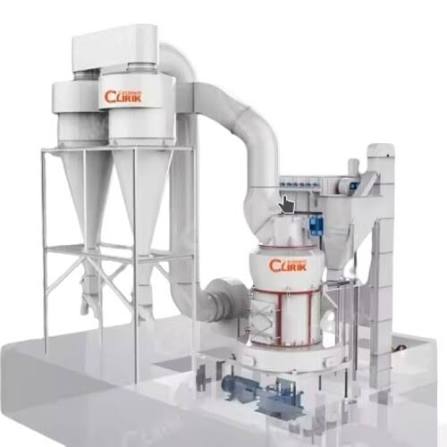
Raymond Mills & Pulverizers

Grinding & Milling

Processed material is ground to exact particle sizes using Raymond mills and pulverizers, ensuring optimal particle distribution, bulk density, and smooth handling properties.

Chemical Reactors

Chemical Reactors

Our 4 dedicated reactors facilitate precision synthesis and controlled chemical transformations for specialty manganese compounds and sulphate formulations.

Laboratory Testing

Quality Testing

Every single batch undergoes lab verification for purity, particle sizing, moisture, and iron content. Full compliance documentation accompanies every dispatch.

Industrial Packaging

Packaging

Finished goods are packed in durable HDPE bags with clear batch labeling, specification seals, and moisture-proof liners. Custom packaging is available on request.
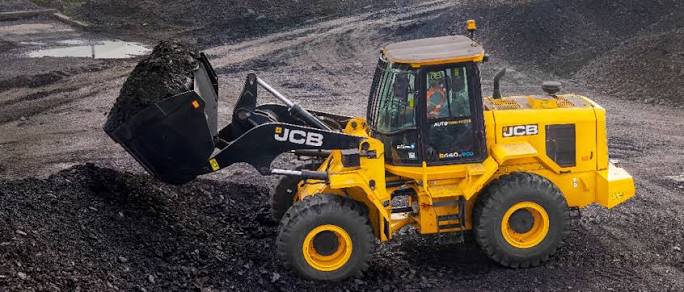
Plant Logistics & Material Handling

Inventory & Logistics

Systematic inventory control ensures uninterrupted year-round availability. Dedicated plant fleet and seamless dispatch coordination guarantee timely global deliveries.

Key Equipment Highlights

Installed heavy machinery and production assets supporting uninterrupted manufacturing excellence

Equipment Quantity Function Capacity
Furnaces 7 Thermal conversion of raw materials 1,800 MT/month
Raymond Mills 4 Grinding to specified particle size 4,000 MT/month
Pulverizers 2 Fine powder production Supporting capacity
Reactors 4 Chemical Reactions Facility operations
Hydraulic Tractors 4 Material handling Facility operations
Loaders 2 Bulk loading/unloading Facility operations
JCB Machines 2 Excavation and movement Facility operations
QUALITY COMMITMENT

Quality is Our Operating Philosophy

At Nijal Mineral and Chemical Industries Pvt. Ltd. (NMACIPL), quality is not a department or a step in the process—it's how we operate. Every decision, every process, and every interaction is guided by our commitment to quality.

PILLAR 01

Rigorous Testing

Our in-house laboratory tests every batch before shipment as an uncompromising quality gate:

  • Product specs: Purity, particle size, density, moisture & iron content
  • Batch consistency: Benchmarked against historical standards
  • Performance characteristics: Application-specific standards

Documented test results accompany every shipment; non-conforming batches are rejected or reprocessed.

PILLAR 02

Process Control

Our furnaces, mills, and support equipment operate under continuous monitoring to keep operations locked in specification:

  • Real-time sensors: Regulating temperature, timing, and atmosphere
  • Material flow meters: Standardizing feed and processing rates
  • Automated logging: Recording complete operational parameters

Modern automation platforms generate an immutable parameter record for each production run.

PILLAR 03

Inventory Management

Rather than rushing to ship freshly processed material, systematic warehousing protocols ensure:

  • Product stabilization: Natural post-production settling and curing
  • Secondary verification: Pre-dispatch lab confirmation
  • Consistent supply: Year-round stock availability without rush cycles

Dedicated warehousing ensures immediate fulfillment capability for urgent customer orders.

PILLAR 04

Batch Traceability

Every single finished product batch carries a unique identifier providing complete end-to-end lineage tracking:

  • Raw materials: Source provenance and incoming lab test records
  • Processing history: Exact production date, operators, and equipment utilized
  • Dispatch details: Quality testing certificates and complete shipping records

Ensures instant, transparent root-cause verification for any customer queries or technical audits.

PILLAR 05

Continuous Improvement

We actively monitor client feedback, industry trends, and internal plant metrics to drive targeted upgrades:

  • Equipment maintenance: Planned overhauls and cutting-edge machinery additions
  • Process refinement: Fine-tuning milling parameters and furnace efficiencies
  • Workforce development: Routine operator training on safety and QA protocols

Operating on the principle that quality is an ongoing journey, not a final destination.

TECHNICAL EXPERTISE

Technical Depth Behind Every Product

Nijal Mineral and Chemical Industries Pvt. Ltd. (NMACIPL) doesn't just manufacture products—we understand manganese chemistry and its applications. This deep expertise informs everything we do.

CUSTOM FORMULATIONS

Product Development

When customers require tailored parameters, our laboratory and technical team formulate precise custom specifications. We understand:

  • Purity Variance: How slight variations in purity affect end-application performance
  • Particle Distribution: How particle size spread impacts powder flow and handling
  • Processing Methods: How distinct thermal and chemical routes modify product structure
  • Application Tuning: How to optimize chemical grades for specific industrial needs
CROSS-INDUSTRY INSIGHT

Application Knowledge

Decades of active collaboration across battery cells, water treatment, ceramics, glass, pharmaceuticals, and agriculture enable us to master:

  • Industry Demands: Strict compliance characteristics required by every sector
  • Root-Cause Solutions: Diagnosing common shopfloor production challenges
  • Use-Case Optimization: Fine-tuning material reactivity for specific client facilities
SCALE & EFFICIENCY

Process Optimization

As production volumes scale or purity specifications tighten, our engineering division helps streamline your downstream operations:

  • Grade Recommendation: Selecting optimal material grades for exact machinery setups
  • Equipment Matching: Adjusting mesh profiles to fit specific pneumatic and hopper systems
  • Cost Optimization: Identifying operational efficiencies without compromising quality
  • Collaborative Solving: Real-time technical support for seamless production continuity
OUR MANUFACTURING LOCATIONS

Strategically Located for Efficient Supply

Integrated manufacturing and commercial operations connecting our primary plant in Gujarat with our corporate export gateway in Mumbai.

PRIMARY MANUFACTURING BASE

Nijal Mineral and Chemical Industries Pvt. Ltd.

📍 Plant: Survey No. 207, Gopipura, Halol, Panchmahal, Gujarat – 389350, India

Location Advantages

  • Halol Cluster: Proximity to core raw material suppliers
  • Logistics Hub: Well-connected to ports, highways & rail network
  • Central Supply: Efficient pan-India bulk distribution
  • Infrastructure: Dedicated power, utilities & skilled workforce

What's on Site

  • 500,000 sq ft comprehensive manufacturing campus
  • 7 Furnaces & 4 Raymond Mills for processing
  • Full in-house batch testing & QA laboratory
  • Organized inventory staging & bulk packing units
  • Dedicated on-site production & plant operations team
500K Sq. Ft. Campus
7 Furnaces
4 Raymond Mills
QA Lab In-House Testing
COMMERCIAL & EXPORT GATEWAY

Nijal Mineral and Chemical Industries Pvt. Ltd.

📍 Office: 25/A Chandawadi, 138 CP Tank Road, Mumbai – 400004, Maharashtra, India

Commercial Advantages

  • Business Capital: Close proximity to major industrial buyers
  • Export Gateway: Fast documentation & direct JNPT port connectivity
  • Financial Hub: Swift LC settlements & trade finance handling
  • Client Relations: Dedicated corporate meeting & contract hub

What's Managed Here

  • Dedicated sales desk for domestic chemical supply
  • Global export documentation & freight routing
  • Nationwide distribution logistics & stock movement
  • Direct customer relationship & key account support
  • Contract specifications review & corporate invoicing
JNPT Port Access
Global Export Routes
B2B Enterprise Hub
PAN-India Distribution
Direct Dispatch & Sales Desk Contact our team for quick quotes, ready batch inventory, and technical COA sheets.
Direct Call +91-9967445399
OUR VALUES & VISION

What We Stand For

Guided by technical integrity, unwavering quality standards, and deep customer collaboration across every facet of our operations.

🎯 OUR MISSION

Mission Statement

To manufacture and supply high-quality manganese-based industrial chemicals that enable our customers' success, supported by technical expertise, reliable delivery, and genuine partnerships.

🔭 OUR VISION

Vision Statement

To be the most trusted manganese manufacturer in India, recognized for quality, reliability, technical depth, and unwavering commitment to customer success.

Our Core Values

01

Quality First

Everything we do is guided by commitment to quality. Not "good enough"—excellent.

02

Customer Partnership

We view our customers as partners whose success is our success. Their problems are our problems.

03

Technical Excellence

We understand our industry deeply and continuously expand that knowledge. Technical depth is a competitive advantage we invest in.

04

Reliability

When a customer places an order, they can depend on consistent quality, on-time delivery, and responsive support. Reliability is foundational to everything we do.

05

Continuous Improvement

We never assume we've perfected our processes. We continuously look for ways to improve quality, efficiency, and customer experience.

06

Integrity

We operate transparently, communicate honestly, and follow through on commitments. Trust is earned through consistent integrity.

The People Who Make Nijal Mineral and Chemical Industries Pvt. Ltd. (NMACIPL)

Founder & Leadership

Ashik Shah

Co-founder

Leading NMACIPL with extensive strategic foresight in manganese manufacturing and plant operations.

Ronak Shah

Co-founder

Guiding organizational foundation, corporate governance, and sustainable business growth across the company’s initiatives.

Team Overview

Operations & Production

Experienced equipment operators and production supervisors trained in furnace operations, grinding systems, and quality protocols. Continuous training ensures expertise remains current.

Quality & Testing

Laboratory professionals trained in chemical analysis, specification testing, and batch verification. They're the gatekeepers of our quality commitment.

Sales & Customer Service

Customer-focused professionals based in Halol and Mumbai who understand our customers' industries and technical requirements. They're the bridge between our manufacturing capability and customer needs.

Technical Support

Engineers and chemists available to discuss applications, troubleshoot issues, and develop custom solutions.

Tell us the grade and the tonnage

Send the assay range, mesh, monthly quantity and delivery port or city. You will get a quote with a lead time, not a brochure.